When an Old Control System Becomes an Operational Risk
Industrial control systems often remain in service for years because they perform their core tasks well. A production line may still run through an older programmable logic controller (PLC), while operators use a supervisory control and data acquisition (SCADA) platform that was installed many years ago. The system may seem reliable, but finding replacement parts, maintaining software compatibility and obtaining technical support can become harder as the equipment ages.
These problems can affect production planning, fault recovery and long term maintenance costs. Older systems may also lack the network controls, data access and reporting tools that modern industrial operations need. For Canadian manufacturers, utilities, food processors and other industrial businesses, a planned upgrade can address these issues without requiring the replacement of every control component at once.
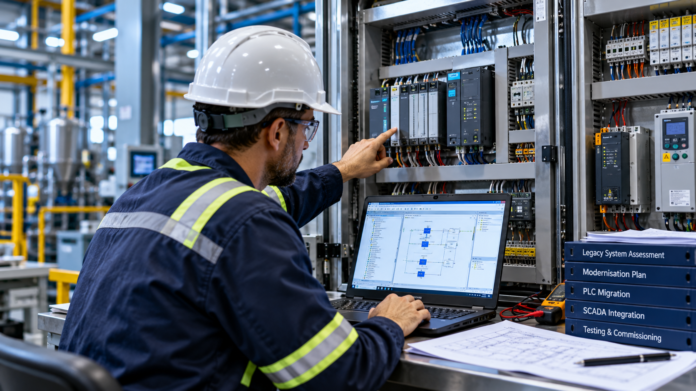
Legacy control system modernisation involves assessing existing equipment, identifying technical limits and updating selected parts of the control environment. The goal is to protect useful assets, reduce operational risk and create a sound path for future automation work. The right approach depends on the condition of the equipment, the process requirements and the cost of interrupting production.
Five Warning Signs That Your Control System Needs Attention
An ageing control system does not always need immediate replacement. However, certain warning signs can show that maintenance alone may no longer be enough. Plant managers and automation engineers should review these signs together, since several small issues can point to a larger problem.
- Replacement parts are hard to obtain. Older PLCs, communication cards, operator panels and other components may no longer have reliable supply channels. If a failed component can stop a production line for several days, the business needs a clear plan for replacement or migration.
- Technical support is limited. Older software may no longer receive vendor support or work with current operating systems. This can make fault diagnosis harder and increase the time needed to restore normal operation after a failure.
- Operators lack useful process data. An older SCADA application may display basic machine status but provide limited alarm history, reporting or trend analysis. Engineers may need to collect records by hand to identify recurring faults or compare performance across shifts.
- New equipment cannot connect easily. Modern machines may use communication protocols that the existing control environment does not support. Additional gateways can help, but too many separate interfaces can make the system harder to maintain.
- Security controls need improvement. Older industrial networks may have weak access controls, limited network separation or outdated software. The National Institute of Standards and Technology’s guide to operational technology security describes security measures for operational technology while accounting for its reliability and safety needs.
A single warning sign does not prove that the system must be replaced. A technical assessment can show which parts remain suitable for service, which need an upgrade and which pose a risk to production.
Upgrade, Retrofit or Replace? Compare the Main Options
The most suitable modernisation plan depends on the role of each component and the cost of failure. Replacing a working PLC may add little value if the main problem lies in the SCADA software. In another plant, an obsolete controller may limit the whole system, making a larger change necessary.
| Modernisation option | Best suited to | Main benefit | Main concern |
| Software upgrade | Existing hardware that remains supported and compatible | Improves selected software functions | Compatibility and testing requirements |
| SCADA platform migration | Older supervisory software with limited support or features | Adds modern monitoring and data tools | Screen recreation and data migration |
| PLC replacement | Controllers with serious support, capacity or reliability issues | Restores access to supported control hardware | Control logic changes and commissioning risk |
| Communication retrofit | Equipment that works but cannot connect to newer systems | Extends data access without full replacement | Gateway limits and protocol compatibility |
| Partial system replacement | A mix of usable and obsolete components | Focuses investment on the main problem areas | More complex integration and documentation |
| Full system replacement | Systems with major technical or operational limits | Provides a new control architecture | Higher cost and greater project scope |
A partial upgrade can make sense when the existing control logic remains stable and the main problem involves monitoring, reporting or connectivity. A full replacement may be more suitable when the hardware is obsolete, spare parts are unavailable and the system cannot meet current process requirements.
The decision should follow a documented assessment rather than the age of the system alone. Engineers should consider production risk, support availability, safety requirements, future capacity and the time needed to test the new design.
PRO TIP
Before approving a full replacement, ask the engineering team to separate the control hardware, supervisory software, communication network and reporting layers. This helps identify which parts can remain in service and which need work. It can also reduce the project scope without leaving critical risks unresolved.
How SCADA Programming Supports Legacy System Upgrades
SCADA programming plays a key role when an industrial business needs to improve monitoring without changing every controller. Engineers can update operator screens, alarm handling, historical data collection and reporting while keeping compatible field equipment in place. The exact scope depends on the existing platform, the available communication drivers and the functions that operators need during each shift.
For example, a food processing plant may have older PLCs that still control its conveyors, pumps and mixing equipment. The local control logic may remain reliable, but the central monitoring application may lack useful production trends and alarm records. A SCADA upgrade could connect compatible controllers to a newer supervisory platform and provide a clearer view of the process.
The engineering team must check that the new software reads the correct signals and uses the right units, limits and alarm conditions. It must also confirm that operator commands work as intended and that the existing control logic continues to perform its approved role. Testing should cover normal operation, fault conditions and recovery from communication loss before the updated application goes live.
This approach can help businesses gain better access to process data while keeping useful control equipment in service. It does not remove the need to replace hardware that has reached its technical or operational limits.
The Role of SCADA System Design in Modernisation
A successful upgrade needs a clear system design before engineers start changing live equipment. The design should show how the existing PLCs, HMIs, SCADA servers, databases and industrial networks fit together. It should also identify which components will remain, which will change and how the new system will communicate with the old equipment during the transition.
Good SCADA system design also protects operator workflows. Staff may rely on familiar screen layouts, alarm colours, equipment names and control sequences. A new application should improve clarity without making routine tasks harder or changing approved operating procedures without review.
Data migration needs the same level of care. Historical records may support maintenance planning, compliance reporting or production analysis. Before moving them, the project team should identify which records matter, confirm their format and decide how much history the new system must retain. The team should then test the migrated data and document any limits.
Security must form part of the design from the start. Industrial networks should allow only the communication needed for approved functions, with access rights based on staff roles. Network separation, controlled remote access, secure backups and a clear change process can help reduce risk. NIST’s Guide to Operational Technology Security provides further guidance on these controls.
How to Limit Downtime During a Control System Upgrade
Production downtime can be one of the main costs of an industrial automation project. An upgrade may require access to control cabinets, changes to communication settings, software migration or tests that cannot take place during normal production. The project plan should account for these limits before the team schedules the work.
A staged migration can reduce the amount of equipment that must be taken offline at one time. Engineers may be able to develop and test parts of the new SCADA application away from the live process, then connect them during an approved shutdown. A parallel setup can also help in suitable cases, although it needs careful control to prevent conflicting commands or inconsistent data.
The following measures can help reduce the risk of a prolonged interruption:
- Record the existing control logic, software versions, network settings and device configurations before making changes.
- Confirm that tested backups and a practical rollback plan are available.
- Prepare the new application and test its key functions before the production shutdown.
- Agree on the shutdown window, responsible staff and restart checks with plant operations.
- Verify alarms, interlocks, communications and operator controls before releasing the system for normal use.
The team should also define clear acceptance criteria. These may include successful communication with all required devices, correct process readings, working alarms, verified control commands and access to the required historical records. A written test record gives the plant a basis for approving the updated system.
No upgrade plan can guarantee zero downtime. The achievable result depends on the existing equipment, the scope of the changes and the options available for testing before installation. A realistic plan makes these limits clear and prepares the team for faults that may arise during commissioning.
A Practical Modernisation Example
Consider a Canadian industrial facility that uses older PLCs and a legacy SCADA application to monitor several production areas. The PLCs still control the process, but the supervisory software has limited reporting functions and no easy way to compare recurring alarms across shifts. The maintenance team also has difficulty finding compatible parts for some network components.
A full replacement might address these issues, but it could require a large investment and a lengthy shutdown. The engineering team could first assess the PLCs, communication network, SCADA software and available spare parts. If the controllers remain suitable for service, the first stage might focus on the supervisory application, selected network components and the collection of process data.
The team could then test the updated application against a defined list of signals, alarm conditions and operator tasks. Once the required checks pass, the new system could be introduced during a planned shutdown. A later stage could replace any controllers that cannot meet the plant’s future requirements.
This example is illustrative, not a reported client project. It shows how a phased plan can address the most pressing issues first while keeping future changes within a clear technical framework.
Selecting a SCADA Development Software Provider
An industrial upgrade needs a team that can assess existing equipment, work with different control platforms and plan changes around production requirements. A suitable SCADA development software provider should be able to explain the proposed design, identify technical risks and document how the new system will be tested.
Ask the team to review the existing PLC models, HMI applications, network layout and software versions before it confirms the project scope. The proposal should identify the work included, the equipment that will remain, the expected shutdown requirements and the support available after commissioning. It should also explain how the team will protect the existing control logic and verify the new application.
Platform experience matters as well. Industrial sites may use systems such as Rockwell FactoryTalk, Siemens WinCC, AVEVA Wonderware, GE iFIX, VTScada or Ignition. The best platform for the project depends on the existing installation, licensing, device compatibility and future support needs. Engineers should confirm these details before committing to a migration plan.
ControlSoft Canada provides industrial automation services that include SCADA programming, system design and legacy system work. Businesses planning an upgrade can contact the team to discuss the current installation, technical limits and project goals.
Frequently Asked Questions
What is a legacy control system?
A legacy control system is an existing industrial control environment that may rely on older hardware, software or communication methods. It can still perform its intended tasks, but support limits, spare part shortages, integration problems or security gaps may make it harder to maintain. A technical assessment helps determine the level of risk and the work needed.
Does an old PLC always need to be replaced?
No. An older PLC may remain suitable if it operates reliably, has adequate capacity and can receive the support needed for safe operation. Engineers should review its condition, spare parts, communication options and future requirements before recommending replacement. The wider control system may need an upgrade even when the PLC can remain in service.
Can legacy SCADA software connect to modern equipment?
In some cases, existing SCADA software can connect to modern equipment through supported drivers, protocol gateways or compatible communication servers. The available options depend on the software version, device protocols and network design. The engineering team must test the proposed connection before relying on it in production.
How can a business upgrade SCADA without replacing every controller?
The team can assess the existing PLCs and replace or update the supervisory layer if the controllers remain compatible with the new design. This may involve updating operator screens, alarms, reporting and data collection. The scope must account for communication limits, testing needs and any control functions that require changes.
What are the main risks of a legacy control system upgrade?
Common risks include incompatible hardware, missing documentation, incorrect signal mapping, lost historical data and unexpected downtime. Security gaps and changes to approved control logic can add further risk. A detailed assessment, tested backups, staged deployment and formal commissioning checks help manage these issues.
How long does a control system modernisation project take?
The time required depends on the number of devices, the complexity of the process, the quality of the existing documentation and the amount of testing required. A small SCADA software update may take far less time than a plant wide PLC replacement. A site assessment is needed to set a realistic schedule.
Plan Your Next Control System Upgrade
An ageing control system does not always require a complete replacement, but it should not remain in service without a clear plan for support, security and future needs. A structured assessment can show which components remain useful, which need an upgrade and how the work can fit within production limits.
ControlSoft Canada can help industrial businesses discuss SCADA programming, control system modernisation and system design requirements. Contact the team to review your existing installation and plan the next stage of your automation system.
Contact ControlSoft Canada to discuss your legacy control system upgrade.